Workflow scenarios/Pre-Operational Sanitation Checks on a Bottling Line
Food & Beverage

Pre-Operational Sanitation Checks on a Bottling Line

How a beverage plant runs pre-operational sanitation checks on phones, with readings checked against limits, photos of failed items and corrective work raised before the line starts.

Pre-Operational Sanitation Checks on a Bottling Line use case cover

Industry context

Picture a beverage plant running several bottling lines: rinsers, fillers, cappers, labelers and the conveyors that feed the packing hall. Between production runs the lines are sanitized, with clean-in-place cycles for the filler and product lines and foam-and-rinse cleaning for conveyors and exterior surfaces. Before product runs again, a pre-operational inspection confirms that the line is clean, correctly reassembled and safe to start.

The inspection is short but dense. Product-contact surfaces are visually clean, with no residue or standing water. The clean-in-place cycle shows as completed. Sanitizer concentration at the final rinse is tested and within its range. Guards are back on, tools are accounted for, nothing glass or brittle has been broken, and the fill-level and cap inspection systems reject their test containers. Only then does the line lead sign the line off for production.

It is also one of the records auditors read most closely. Whether the plant is audited by customers, a certification body or a regulator, the question is the same: can you show, line by line and day by day, that the checks your food safety plan calls for were done, by whom, and what happened when one failed?
The challenge

On paper, the pre-op sheet lives on a clipboard at the line. It is filled in quickly, often by the same person who has just finished the sanitation and wants the line running. Items are ticked in a column, the sanitizer reading goes in a box with no reminder of the acceptable range, and the sign-off is a signature at the bottom. When an item fails, the response is written in the margin: "guide rail re-cleaned", "called maintenance".

The problems show up later. A margin note saying maintenance was called says nothing about whether the damaged guide rail was ever repaired, and the next morning's sheet may record the same problem. Quality reviews the sheets at the end of the week, long after anything could be done about them. And when an auditor samples a month of records, missing signatures, illegible readings and ticks without a recorded value become findings in their own right.

There is a cost at the start of every shift, too. When a failure is found late, or found and not escalated, the line waits while someone tracks down a technician by radio. The pre-op check is supposed to protect the start of production. Too often it delays it without protecting it.

The solution

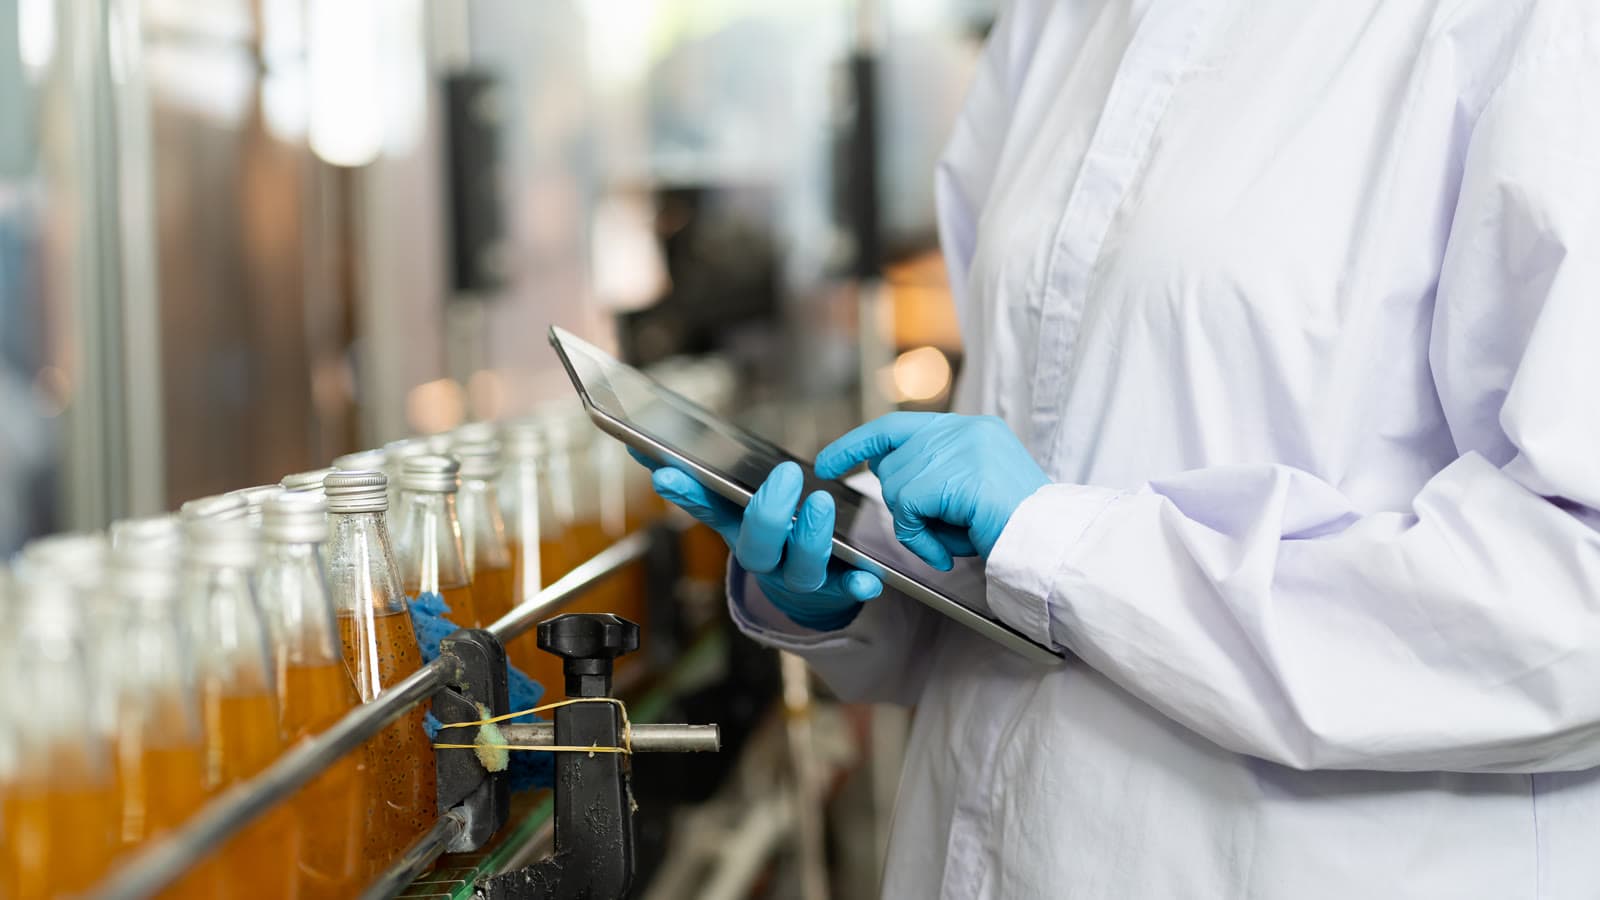
In this scenario, the plant moves each line's pre-op sheet into Vardian as a digital form, opened on a phone or tablet at the line. The items stay the same; what changes is what the form does with them. Readings such as sanitizer concentration carry their acceptable range, so a value outside it is flagged the moment it is entered, while the person who took it is still standing at the rinse point and can re-test. Each failed item is recorded with a photo and a short note.

A failed item that needs maintenance, such as a worn guide rail, a leaking valve or a damaged guard, becomes a corrective work order straight from the inspection, linked to that piece of equipment and to the check it came from. Maintenance sees it as soon as it is raised rather than hearing about it on the radio, and when the repair is signed off it becomes part of the equipment's history. Items that need re-cleaning go back to sanitation and are re-checked on the same form.

The sign-off at the end records who completed the inspection and when. Quality sees completed and failed pre-ops as they happen, line by line, instead of a stack of sheets on Friday. Because every record is stored against the line and its equipment, an auditor's request for a month of pre-op records is answered from the system, not from a filing cabinet.

Implementation

The rollout starts with one line and its existing pre-op sheet, converted as it is. The temptation to improve the checklist during conversion is worth resisting; it is easier to change content after a few weeks of real use, when the team can see which items actually fail. The free pre-operational sanitation inspection checklist is a useful cross-check for anything the current sheet misses.

The important decisions are not about software. Quality and production agree which failed items stop the start-up and which can be corrected while the line runs, following the plant's own food safety plan. They agree who signs the line off and who can override a failed item. Maintenance agrees how corrective work raised from pre-op is prioritized against the rest of the backlog, so a guide rail found before the morning start is not queued behind next month's preventive work.

The first line runs on the digital form with the paper sheet kept as a fallback for a couple of weeks. Once the line leads trust it, the paper goes, and the other lines follow one at a time. Changeover checks are a natural next step, using the same approach with a line clearance checklist.

The results

The first change line leads notice is that a failed item now goes somewhere. A photo and a work order reach maintenance while the line is still being prepared, so repairs start before production is delayed rather than after it. Out-of-range readings are caught and re-tested at the rinse point instead of being discovered in the weekly review.

Quality's work shifts from collecting and checking paper to reviewing exceptions. Instead of reading every sheet, the team looks at failed items, overrides and repeat problems. The same guide rail failing on the same line becomes visible as a pattern once each finding is recorded against the equipment rather than on a sheet filed by date.

Audit preparation changes most. Records are complete by design: every item has a value, every failure has a photo and an outcome, and every sign-off has a name and a time. If your plant runs pre-op checks on paper today, a useful first step is to pull one month of sheets for one line and count how many failed items have a recorded outcome. Then see how quality teams use Vardian for checks, nonconformance and corrective action.

See Vardian in your operation

Bring a real frontline, maintenance, production, safety, quality, or facility workflow. We’ll show how Vardian can connect it.